As semiconductor components become smaller and production volumes rise, packaging accuracy matters at every step. The World Semiconductor Trade Statistics (WSTS) Fall 2024 forecast projected global chip sales of $626 billion in 2024 and $697 billion in 2025. These figures describe the wider market, not carrier-tape demand directly. Still, they show why manufacturers need packaging processes that protect components and maintain consistent output.
An Automatic Carrier Tape Forming Machine heats a plastic web, forms pockets, and prepares the tape for component loading and cover-tape sealing. Operators must match the material, pocket dimensions, forming temperature, and line speed to the component. A small mismatch can deform a pocket or affect pick-and-place accuracy. Small errors compound. This guide explains how to set up the machine, check its key parameters, and inspect formed tape during production. It also covers practical details, such as confirming pocket depth, monitoring web tension, and checking the first pieces before running a full reel.
SEMI reported that global semiconductor manufacturing equipment sales reached $117.1 billion in 2024. That broader investment figure does not measure carrier-tape machinery, but it reflects ongoing attention to production capacity and process control. In 2026, machine selection and operating conditions should still be based on actual component drawings, material specifications, and trial results—not a generic recipe. There is no universal setting. Careful records and repeatable checks help teams identify problems early, though they cannot replace sound operator judgment.
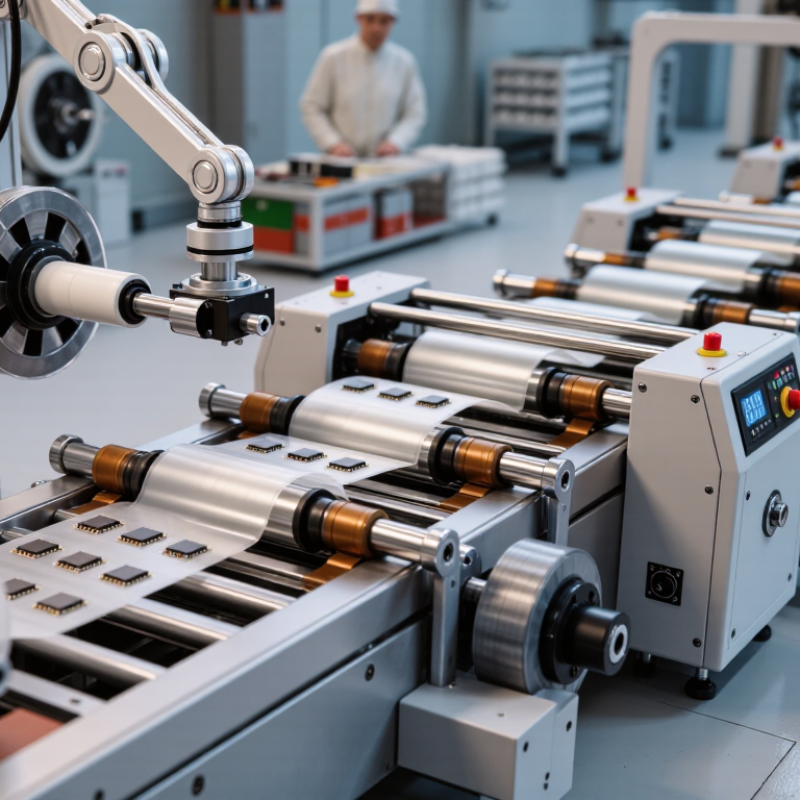
An automatic carrier tape forming machine shapes a continuous plastic strip into pockets that hold electronic components during handling. The process starts at the unwind unit, where a reel feeds material into the machine. A tension controller keeps the strip steady; uneven tension can shift pocket positions. The heating station softens the plastic before a forming station presses it into a mold using vacuum or air pressure. Small details matter. Heat that is too low may leave shallow pockets, while excess heat can distort the strip.
The punch station creates sprocket holes along the tape edge, allowing precise indexing. A take-up unit then winds the formed tape onto a reel. Depending on the configuration, sensors or a camera check pocket shape, hole spacing, and material alignment. Some production lines also include cover-tape sealing, but this may be a separate module. Operators should confirm that the mold, tape width, and pocket dimensions match the component specification before running a full reel. In practice, setup readings do not always tell the whole story; a short trial run can reveal wrinkles or inconsistent pocket depth that a display may miss.
Start with the tape material specified by the product drawing. Confirm its polymer type, width, thickness, and reel condition before loading it. Dust, curled edges, or uneven thickness can cause poor feeding and inconsistent pockets. Keep material stored as recommended for its grade, especially when moisture or static may affect processing. Check that the roll unwinds smoothly, without snagging.
Inspect the forming tooling before installation. Look for residue, worn edges, or damage around the cavities and punch areas. Verify that pocket dimensions, pitch, and alignment match the job requirements. Set feed pitch, forming temperature, dwell time, pressure, and cooling according to the machine and material specifications. Avoid copying settings from a different material. Even a small mismatch can distort pocket walls. Run a short trial, then measure sample pockets and check the tape’s flatness. A rushed setup may look fine at first.
Tips: Change one setting at a time during adjustment. Keep a record of the material lot and final settings. Check samples after the machine reaches stable operation, not only at startup. If results vary, pause and inspect the feed path and tooling before increasing heat or pressure. That extra check can prevent wasted tape. Some machines behave differently across shifts; the reason is not always obvious.
How to Use Automatic Carrier Tape Forming Machine in 2026?
Configure Forming Parameters for the Carrier Tape Design
Start with the component drawing, then set pocket length, width, depth, pitch, and cover-tape area. Match sprocket-hole spacing and edge margins to the feeder specification. WSTS’s Autumn 2024 forecast projected global semiconductor sales of $697 billion in 2025, underscoring the scale of components that packaging lines must handle. That figure is market context, not a forming-machine target. Small changes matter. A pocket that looks acceptable can still let a tiny component rotate during feeding.
Set forming temperature, pressure, cooling time, and line speed for the tape material and pocket geometry. Run a short trial, then inspect several pockets with calipers and a sample component. Check for rounded corners, thin walls, inconsistent depth, and smooth release. Adjust one parameter at a time; changing heat and speed together can hide the cause of defects. Record the working recipe, material lot, and inspection results. A stable setting may still need review when material thickness or ambient conditions change.
Tips: Use a real component as a fit check, not only a drawing. Confirm pocket dimensions against the applicable carrier-tape specification, such as EIA-481. Recheck the first pockets after every setup change. A quick visual check helps, but it cannot replace measurement.
Configure the forming setup around the carrier-tape design. The chart shows common nominal pocket-pitch options in millimeters.
Select the indexing pitch to match the component layout and tape drawing, then set the forming tooling and process parameters for the tape material and pocket geometry. These are format examples; confirm the required dimensions against the component drawing and applicable carrier-tape specification.
Before production, check that the carrier tape reel is correctly oriented and the forming area is clean. Confirm the material type and enter the approved settings for temperature, feed speed, and forming depth. Thread the tape along the marked path, keeping it flat and centered. Start with a short trial run at a reduced speed. Inspect several pockets for even edges, consistent depth, and clean cuts before increasing output. A small adjustment may still be needed; real machines rarely behave perfectly on the first pass.
During production, watch the tape as it moves through the heater and forming station. Look for sideways drift, wrinkles, uneven pockets, or changes in pitch. Use the machine’s gauges or inspection camera, and compare samples with the specified dimensions. Keep the first strip for reference. Check samples at intervals set by your quality plan, and record settings when results are stable. If defects appear, pause the line and investigate the material path, temperature, or tooling instead of making several changes at once.
Tips: Keep the work area clear and avoid reaching into moving parts. Note unusual noise or heat, even if the tape still looks acceptable. Small clues matter.
Example production control plan for a 12 mm carrier tape with 8 mm pocket pitch. Pocket dimensions and process settings must follow the approved product drawing, material supplier instructions, and machine limits; the sample figures below are not universal specifications.
| Production Stage | Operator Action | What to Monitor | Example Check or Acceptance Basis | Response to an Issue |
|---|---|---|---|---|
| 1. Prepare the job | Confirm the work order, tape width, pocket layout, material type, and approved forming recipe. Check that guards and emergency stops are functional. | Job identity, drawing revision, material specification, machine status, and safety interlocks. | Work order and drawing revisions match; required guards and interlocks are in place before operation. | Do not start if documents, material, or safety checks do not match the job requirements. |
| 2. Load the material | Mount the carrier-tape material roll in the correct orientation. Thread it through the guides and forming station according to the machine instructions. | Roll alignment, web tracking, material surface condition, and correct feed direction. | For this example, verify that the specified tape width is 12 mm and that the web tracks centrally without wrinkles or edge damage. | Stop and realign the roll or replace damaged material before forming. |
| 3. Set up the forming recipe | Enter the approved recipe for the material and pocket design. Allow the forming station to reach its specified operating condition before feeding production material. | Recipe selection, heater-zone readings, forming pressure or vacuum (as applicable), and warm-up stability. | Use the approved material-specific recipe and the machine manufacturer’s operating limits; do not substitute a generic temperature or pressure. | Check recipe selection, sensors, and utilities. Resume only after settings stabilize within the approved limits. |
| 4. Start a trial section | Run a short length at the approved start-up speed. Keep the output identified as a trial until the first-off inspection is accepted. | Feed stability, pocket appearance, web tracking, and indexing against the selected pitch. | Example layout: nominal pocket pitch of 8.00 mm; verify against the drawing tolerance for the actual job. | Pause production if pockets are incomplete, distorted, misplaced, or consistently off-pitch; correct the setup and repeat the trial. |
| 5. Inspect first-off pockets | Measure the first formed section using suitable calibrated inspection equipment. Compare results with the product drawing. | Pocket length, width, depth, pitch, pocket position, and tape condition. | Record actual measurements and confirm every checked characteristic meets its drawing tolerance. Pocket dimensions are design-specific. | Adjust only within the approved process instructions, then form and inspect another trial section before releasing production. |
| 6. Release production | After first-off approval, run the machine at a stable rate within its rated capacity. Keep the approved recipe and material lot traceable. | Line speed, feed consistency, forming-station readings, and any machine alarms or stoppages. | Maintain the approved production recipe; record the material lot, recipe identification, start time, and first-off approval. | Stop and investigate repeated alarms, unstable feed, or changes in formed-pocket quality. |
| 7. Monitor during the run | Inspect samples at the frequency set by the control plan and after relevant events such as a material splice, adjustment, or extended stoppage. | Critical pocket dimensions, pitch, web tracking, surface defects, and forming consistency. | Compare sampled results with the drawing and the control plan. Log measurements, time, and any adjustments. | Contain product produced since the last accepted check if a result is out of tolerance; correct the cause and re-inspect. |
| 8. Handle a process interruption | Follow the machine’s restart procedure after a jam, power interruption, material change, or extended stop. | Material position, temperature recovery, recipe status, and the quality of the first pockets after restart. | Recheck the first formed section after restart according to the control plan before returning to normal production. | Segregate questionable output and obtain quality approval where required by the site procedure. |
| 9. Finish and record the run | Stop the machine using the normal procedure, identify the finished reel, and complete production and inspection records. | Reel identification, quantity, material lot, inspection results, rejects, and downtime. | Records should link the finished reel to its job, material lot, recipe, and inspection history. | Label and hold any reel with incomplete traceability or unresolved quality concerns. |
Before running an automatic carrier tape forming machine, inspect a sample from the first few meters. Check pocket shape, pitch, edge alignment, and surface condition under good lighting. Look for cracks, burrs, uneven pockets, or tape that curls after forming.
Small flaws matter. Compare measurements with the job specification, and record any drift rather than relying on memory. If dimensions vary, pause the line and check material loading, heating, and forming pressure before continuing.
Tips: Keep a small sample from each setup. Use a clean ruler or gauge, and inspect both sides of the tape. A quick visual check can miss shallow pocket defects.
At shutdown, follow the machine’s operating instructions and isolate power before cleaning or servicing. Allow heated parts to cool. Remove tape scraps and dust with suitable tools; avoid pushing debris into guides or sensors.
Check rollers, forming surfaces, fasteners, and cable connections for wear or looseness. Lubricate only points specified for routine service. Record unusual noise, sticking, or temperature changes for the next operator.
It is easy to rush this step at the end of a shift, and that is when small maintenance issues can go unnoticed. If a part looks damaged, do not guess at a repair; consult qualified service personnel.